

Cut-Off Die Design for Thin-Gauge Steel Door Frame Profiles
Door Frame Roll Forming Cut-Off Deformation Controlling
In door frame roll forming production, cut-off deformation can compromise the profile quality even after precise forming. Thin-gauge steel sections are particularly vulnerable to cutting forces, which may cause flared flanges, crushed corners, excessive burrs, twisted ends, and uneven cut surfaces. These defects can affect the dimensional accuracy and final assembly of door frame profiles.
Proper cut-off die design and a well-controlled cutting sequence are essential to prevent deformation. By supporting the profile during cutting and distributing the cutting forces evenly, the system helps maintain square ends, clean edges, and consistent profile geometry. This ensures accurate alignment during welding and assembly while reducing fitting problems during installation.
Table of Contents
The Cut-End Problem in Steel Door Frame Production
Cut-end defects in thin door frame sections fall into a few recognizable patterns. The table below summarizes each defect, its root cause, and the condition to check first.
| Defect | Root Cause | What to Check |
|---|---|---|
| Flared flanges | Shear pushes unsupported material sideways instead of fracturing it cleanly; narrow flanges have little material to absorb blade side thrust | Flange support in the die; die clearance; rake angle |
| Crushed corners | Return bend or hem collapses under off-axis clamp or die pressure | Clamp loading direction; clamp timing; internal support of return bends |
| Edge burr | Clearance too small or too large for actual sheet thickness, changing the fracture mode | Actual sheet thickness versus die clearance setting; blade sharpness |
| Twisting / out-of-square ends | Asymmetric force, uneven clamping, or a blade that engages the section progressively | Force symmetry; clamp sequencing; rake angle |
The downstream consequences are practical. Out-of-square ends reduce the contact area at miter joints, forcing assemblers to compensate with weld fill or grinding. Burrs create handling hazards and interfere with gaskets, seals, and hardware fit. Flared flanges change the effective profile width, so a frame that measured correctly upstream may not close properly during assembly. For production engineers, these door frame roll forming cut-off deformation defects also increase scrap and slow the stacking and packaging step.
Profile Geometry and Thin-Wall Behavior at Cut-Off
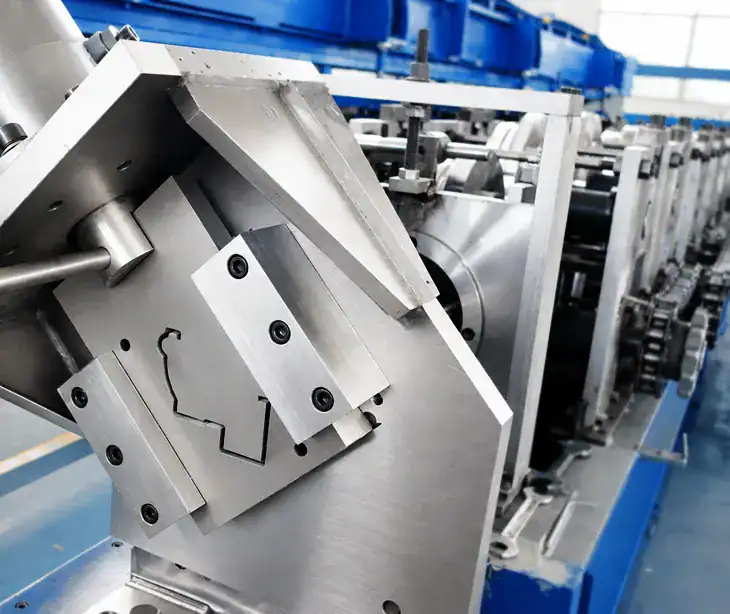
Door frame sections are not simple open channels and thin gauge door frame roll forming is not a simple proudction. They typically combine narrow flanges, a jamb face or stop leg, and one or more return bends or hems. Each of these features changes how the section behaves under shear. Thin gauge material has limited bending stiffness, so the shear load is not distributed evenly across the section. The blade tends to force the weakest leg first, and the profile rotates slightly before the opposite side fractures.
Return bends and hems are especially sensitive. They are stiff locally but enclose small radii, and they can fold or open if a clamp loads them off-axis. Narrow flanges have little material to absorb the blade’s side thrust, so they flare or bow outward. Allowable die clearance therefore has to be tighter than it would be for a heavy open section, because a wider clearance that works fine on thick material allows thin walls to pull into the die gap and tear instead of shearing.
How Shear Clearance and Rake Angle Affect Cut-End Quality
Shear clearance is usually expressed as a percentage of material thickness per side. In thin-gauge door frame roll forming, clearance has to be held in a narrow band. Too little clearance produces secondary shearing, high blade load, and a rough, torn edge. Too much clearance lets the material bend into the gap, creating a rolled edge, a large burr, and a slightly bell-mouthed section.
Rake angle, the slope of the blade edge across the section, controls how the cut progresses. A blade that enters the full section at once can shock the profile and distort it. A modest rake spreads the cut so the fracture starts at one side and moves across, which lowers peak force and reduces flaring. Excessive rake, however, pushes material along the profile axis, which is one common cause of cut end squareness roll forming issues, especially when a long, unsupported leg is the first thing the blade contacts. In practice, the goal is a progressive but controlled fracture, matched to the section’s stiffest feature.
Support and Clamping Inside the Cut-Off Die
Most cut-end deformation is really a support problem, and door frame profile cutting deformation can’t pass it neither. When a flange is unsupported at the moment of shear, it has nowhere to go but outward or sideways. Die blocks, mandrels, and telescoping inserts that fill the internal cavity of the profile restrict that movement. A well-supported die holds the flanges and the return bends in position while the blade passes through, so the material fractures rather than bends.
Clamp timing matters as much as clamp force. If the clamp closes before the blade engages, the section is rigid at the moment of shear. If the clamp closes late, the profile shifts slightly and the cut end is out of square. Sequencing the clamps to hold both the flange and the internal return surface, then releasing only after the blade has cleared the section, is a reliable way to reduce crushed corners and flared flanges. It also helps when material thickness varies from coil to coil.
Tooling and Setup Implications for Door Frame Roll Forming Lines
Cut-off die design interacts directly with line setup. Coil thickness variation changes the effective clearance, so a die that cuts well at nominal gauge may produce burrs or distortion on the thin or heavy end of the tolerance. Changeover between door frame sizes is also affected, since support blocks and inserts often need to be swapped or repositioned, and the rake may need adjustment if the section stiffness changes.
Commissioning checks should include cut end squareness, flange flare, burr height, and twist, measured at the start, middle, and end of a coil run. These checks should be repeated after the first tool changeover, because small differences in shim, clamp position, or blade sharpness are easier to correct early than after the line is in full production. Information on shear and cutting practice from The Fabricator can help engineers confirm accepted shop practice for thin-gauge cutting.
Specifying a Cut-Off System for Thin-Wall Door Frames
When specifying new equipment or resolving an existing cut-end quality problem, buyers and production engineers should focus on a few configuration questions rather than broad machine features.
- Does the die support the flanges, return bends, and internal cavity of the specific door frame section being run?
- Is shear clearance adjustable, and is it stated as a percentage of the expected material thickness range?
- Is the rake angle selectable or fixed, and does it match the stiffness of the section?
- Are clamps sequenced to close before the blade engages and release after it clears?
- Is the cut-off die design of the steel door frame cut-off die design able to accommodate planned section changes without a full rebuild?
- Is the door frame cutoff tooling built with enough adjustment to correct flare, burr, and squareness during commissioning?
Buyers should also confirm how the vendor defines acceptance for cut end squareness and burr height, and how those checks are performed on the actual line. A clear acceptance check is more useful than a broad performance claim.
Thin gauge door frame roll forming rewards a cut-off die that is matched to the specific section geometry rather than one that simply fits the line. The controlling factors are die clearance, rake angle, internal support, and clamp timing, and they interact. Adjusting one without considering the others usually moves the defect rather than removing it. For engineers chasing door frame roll forming cut-off deformation in production, working through these four variables in sequence is a reliable way to reach consistent, square cut ends.
Frequently Asked Questions
What information is needed to quote a cut-off die? ›
Provide a detailed profile drawing with flange widths, return bend radii, and hem dimensions, plus the material grade, coil thickness range (not just nominal), and coil width. Also state your required cut end squareness and burr height acceptance criteria, target line speed, cutting method preference, and whether the die must handle multiple door frame sizes. This lets the supplier match shear clearance, rake angle, and internal support to your actual section rather than a generic profile.
How do I set shear clearance for thin door frame sections? ›
Shear clearance is normally expressed as a percentage of material thickness per side, and thin-gauge sections need a tighter band than heavy sections. Verify the actual sheet thickness at the thin and heavy ends of your coil tolerance, since the effective clearance shifts with gauge. Too little clearance causes secondary shearing, high blade load, and torn edges, while too much lets material pull into the gap, creating rolled edges and large burrs. Confirm the die allows fine clearance adjustment within your thickness range.
When should rake angle be adjustable rather than fixed? ›
Adjustable rake is useful when you run several door frame sections of different stiffness, or when a long unsupported leg is the first feature the blade contacts. Rake spreads the cut progressively, lowering peak force and reducing flaring, but excessive rake pushes material along the profile axis and hurts squareness. If your product mix is stable and well defined, a fixed rake matched to that section can be simpler. Discuss your changeover plans with the die supplier before deciding.
How should clamps be sequenced inside the cut-off die? ›
Clamps should close and secure the flange and internal return surfaces before the blade engages, then release only after the blade has fully cleared the section. Closing late lets the profile shift slightly, producing out-of-square ends. Closing early without adequate internal support can crush return bends and hems. Ask the supplier to document the clamp sequence and confirm it can be tuned during commissioning, especially if coil-to-coil thickness variation is expected in production.
Can one cut-off die handle several door frame sizes? ›
Often it can, but it depends on how similar the sections are. Support blocks, mandrels, and telescoping inserts usually need to be swapped or repositioned between sizes, and rake may need adjustment if section stiffness changes. Ask whether the die is designed for planned section changes without a full rebuild, how long a changeover takes, and which components are size-specific. Provide your full size list and changeover frequency so the supplier can design for it.
What cut-end checks should be done during commissioning? ›
Measure cut end squareness, flange flare, burr height, and twist at the start, middle, and end of a coil run, since thickness variation along the coil changes the effective clearance. Repeat the same checks after the first tool changeover, when shim, clamp position, or blade sharpness may have shifted. Record the results against agreed acceptance criteria rather than a general performance claim. Early correction of small deviations is far easier than fixing them in full production.
What causes flared flanges on thin door frame cuts? ›
Flared flanges usually mean unsupported material is being pushed sideways by the blade instead of fracturing cleanly. Narrow flanges have little material to absorb blade side thrust, so they bow outward. Check flange support inside the die, die clearance relative to actual sheet thickness, and rake angle. Because these factors interact, adjusting only clearance or only rake often moves the defect rather than removing it. Work through support, clearance, rake, and clamp timing in sequence for a stable result.
