
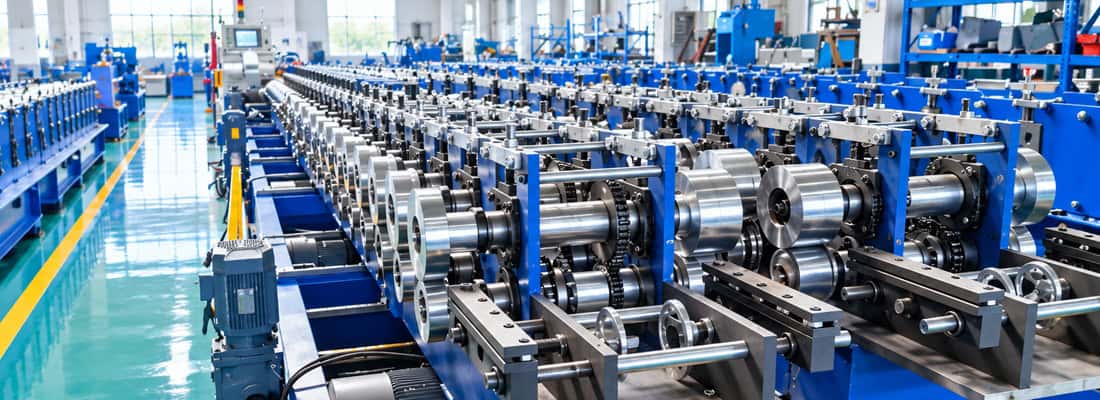
Roll Pass Design for Perforated Cable Tray Profiles
Perforated Cable Tray Roll Forming: How Roll Pass Design Maintains Flange Stability Around Pre-Punched Holes
Perforated cable tray profiles present a distinct challenge in perforated cable tray roll forming. Unlike solid strip, pre-punched holes remove material that would normally help distribute bending stress, leaving isolated ligaments of steel between openings. These weakened zones alter how the strip responds to each forming station, and if the roll pass design does not account for them, manufacturers can see flange distortion, poor hole-edge quality, and dimensional inconsistency. This article examines how perforation patterns affect strip stiffness and how roll tooling, bend sequencing, and tension control must be adapted to maintain stable production.
Table of Contents
How Perforations Change Strip Stiffness in Cable Tray Roll Forming

When a cable tray web or flange is perforated, the remaining material carries the full forming load. The punched openings create narrow bridges of steel that have much lower resistance to local bending than a continuous surface. During incremental forming, these bridges can yield prematurely, allowing strain to concentrate at the edges of the holes rather than distributing smoothly across the profile width.
This reduction in local stiffness is most noticeable when the perforation pattern extends close to a planned bend line. A solid strip will fold predictably around the bend radius because the material on both sides of the bend supports the transition. With holes present, the strip may instead distort at the nearest opening, pulling the web out of plane or creating a wavy edge along the flange. The effect is not constant across the profile either; the open-area ratio determines how much stiffness remains at any given cross-section, so a strip that is heavily perforated in the center but solid near the edges will behave differently than one with uniform perforation.
Mapping Perforation Position, Pitch, and Open-Area Ratio Before Pass Design
The first step in designing a reliable process is to map the perforation layout relative to the final profile geometry. The designer must know the exact position of each hole row in relation to bend lines, the distance from hole edges to the strip edge, and the pitch between openings. This information is typically supplied as a flat pattern drawing or CAD data from the profile specification, as defined by standards such as those from the National Electrical Manufacturers Association (NEMA) for cable tray systems.
The critical parameter is the open-area ratio at each longitudinal section. If a bend line runs through a zone where the open area exceeds roughly 30–40 percent, the remaining bridge width may not provide sufficient material to form a clean radius. In such cases, the designer must either relocate the bend away from the perforation, change the sequence of bending, or confirm with the customer whether the hole pattern can be adjusted. Edge distance is equally important; holes that sit too close to the strip edge leave a narrow margin that can tear or flare during flange forming.
Sequencing Bends Around High-Open-Area Zones
Once the perforation layout is understood, the flower pattern can be arranged to avoid forming directly on the most weakened sections. A common strategy is to complete the initial bends in solid areas of the strip first, creating a partially shaped channel that adds stiffness before the forming passes move into perforated regions. This approach lets the already-formed sections carry the load while the bend progresses through areas with higher open area.
In practice, this means the first forming stations may only work the outer edges of the profile where the material is solid, establishing the flange orientation before the web is shaped. If the web itself carries holes, the bend at the web-to-flange junction may be formed in two or three light passes rather than a single aggressive fold. Partial forming reduces the risk of localized buckling because each station removes only a small amount of the remaining bend angle, giving the weakened material less opportunity to collapse under load.
Overbend and Springback Compensation Around Punched Flanges
Springback behavior in perforated strip is not uniform across the profile. In a solid flange, the entire width resists elastic recovery, producing consistent springback that can be compensated with a fixed overbend angle. When holes interrupt the flange, the remaining material has a different stress distribution after bending. The bridges between holes may be overstressed while the material adjacent to openings retains more elasticity, leading to inconsistent final angles along the length of the profile.
For this reason, overbend settings must be evaluated stage by stage rather than applied as a single global adjustment. If a particular flange shows a larger springback near a row of holes, that station may need a slightly higher overbend than a station forming a solid section. In severe cases, a calibration pass at the end of the line can help normalize the angle, but this only works if the preceding stations have not introduced permanent distortion. The roll tooling designer must also consider that the effective bend radius will be influenced by the hole edges acting as stress concentrators, potentially requiring a larger radius to avoid cracking at the corners of the perforations.
Roll Tooling Clearance and Contact Control at Hole Bridges
The thin bridges between perforations are vulnerable to damage from roll contact. If the rolls exert excessive pressure on these narrow sections, the tooling can mark the surface, smear the edges of the holes, or even flatten the bridge, altering the profile geometry. Roll clearance must therefore be set carefully to avoid crushing the material while still ensuring sufficient contact to drive the strip forward.
One effective approach is to use rolls with a slightly larger diameter on the sections that contact hole bridges, distributing pressure over a wider surface area. Alternatively, the designer can add a small relief in the roll face so that contact occurs primarily on the solid margins of the strip rather than directly over the perforated zone. This reduces the chance of marking while maintaining the forming force needed to shape the profile. The roll material and surface finish also matter; a polished surface with a low friction coefficient will slide over the hole edges more smoothly, reducing the tendency to pick up or smear material.
Feeding, Leveling, and Tension Control for Punched Cable Tray Strip
The perforations affect not only the forming stations but also the way the strip feeds through the line. A punched web has less rigidity, making it more susceptible to camber and twist when subjected to uneven tension. If the decoiler or the leveler pulls harder on one edge of the strip than the other, the weakened material will bow laterally, causing the profile to emerge with a curve along its length.
To manage this, the line should maintain low and consistent tension between stations. A strip with a high open-area ratio may need less overall tension than a solid strip to avoid stretching the bridges between holes. The leveler plays a particularly important role; it must flatten the strip without overworking the areas around the perforations. If the leveler applies too much pressure, it can deform the hole edges before forming even begins. In practice, operators should monitor the strip for signs of edge wave or center buckle after the leveler and adjust the roll gap or tension settings incrementally until the strip runs flat and straight.
Commissioning Checks for Perforated Cable Tray Profiles
When commissioning a new perforated cable tray roll forming line, the verification process should focus on the areas most likely to be affected by the perforation pattern. Start by checking flange squareness at several points along the profile length, not just at the cut ends. Use a square and a straightedge to detect any gradual twisting or angling that may occur as the strip passes through the forming stations.
Also inspect the hole edges for signs of distortion, such as burrs, smearing, or elongation. A hole that was round in the flat strip but becomes oval after forming indicates that excessive tension or roll pressure is stretching the material. Check the distance from the outermost holes to the flange edge to confirm that the bend has not pulled material inward. Run the line at a slow speed initially and visually inspect the profile at each station to see where any deviation first appears. Corrective adjustments should be made one parameter at a time, whether that means changing roll clearance, modifying tension, or altering the overbend angle at a specific station.
The commissioning checks below summarize the main inspection points, the conditions to look for, and the adjustments that address each type of deviation.
| Inspection Point | What to Check | Likely Cause and Corrective Action |
|---|---|---|
| Flange squareness | Gradual twisting or angling along the profile length, not just at the cut ends | Uneven forming forces; adjust roll clearance or overbend angle at the affected station |
| Hole edge quality | Burrs, smearing, or elongation of the hole shape | Excessive tension or roll pressure stretching the material; reduce tension or roll pressure |
| Hole-to-edge distance | Distance from outermost holes to the flange edge | Bend pulling material inward; modify bend sequencing or roll geometry to control material flow |
| Strip flatness after leveler | Edge wave or center buckle | Leveler overworking perforated areas; adjust leveler roll gap or tension settings incrementally |
Corrective adjustments should be made one parameter at a time, monitoring the effect before changing another setting. For a cable tray manufacturer, the goal is not simply to produce a profile that matches the drawing most of the time, but to achieve repeatable results across long production runs. By recognizing that perforations change the mechanical behavior of the strip, and by applying a roll pass design that respects those changes, a forming line can produce stable, dimensionally accurate profiles with clean holes and consistent flange angles.
Frequently Asked Questions
What should buyers specify about the hole pattern before quoting? ›
Buyers should provide a precise flat-pattern drawing showing hole row positions relative to planned bend lines, hole pitch, edge distances, and open-area ratio. This data is essential for roll pass design because it determines where strip stiffness will be reduced. Without this information, tooling may be incorrectly sequenced, leading to flange distortion or poor hole-edge quality during perforated cable tray roll forming.
How does open area affect flange forming around holes? ›
High open-area zones — typically above 30 to 40 percent at a bend line — leave narrow steel bridges that yield prematurely under forming stress. Instead of distributing bending strain evenly, the strip distorts at the nearest opening, causing wavy edges or out-of-plane web movement. The designer must either relocate or sequence bends to avoid these weakened sections or confirm if the hole pattern can be adjusted.
What bend sequence prevents distortion in perforated profiles? ›
The flower pattern should form solid areas first to add stiffness before shaping perforated zones. That often means establishing outer flange angles in early stations, then bending web-to-flange junctions in two or three light passes later. This reduces localized buckling by minimizing the bend angle imposed at each station where the strip has lower resistance to collapse.
Why is springback different where holes interrupt the flange? ›
Material bridges between holes can become overstressed, while sections adjacent to openings retain more elasticity. This creates inconsistent final flange angles along the profile length. Fixed global overbend compensation is therefore unreliable. Each station should be evaluated independently, and a calibration pass may help only if earlier stations have not introduced permanent distortion.
What roll clearance is safest around thin hole bridges? ›
Rolls must not crush narrow bridges between perforations, as excessive pressure can mark the strip, smear hole edges, or flatten the bridges. Effective strategies include using rolls with slightly larger diameters at contact points to spread pressure, or adding relief in the roll face so contact occurs mainly on solid strip margins. Polished low-friction roll surfaces also reduce marking.
How should tension be managed with punched cable tray strip? ›
Punched strip has less rigidity than solid material, making it prone to camber and twist under uneven tension. Operators should maintain low, consistent tension between stations so the bridges between holes are not stretched. The leveler must flatten the strip without overworking perforated zones; check for edge wave or center buckle and adjust roll gap or tension settings incrementally.
Which commissioning checks matter most for perforated tray profiles? ›
Focus on flange squareness along the entire profile length, not just at cut ends. Inspect hole shapes for burrs, smearing, or oval elongation, which indicate stretching from excessive tension or roll pressure. Verify the distance from outer holes to flange edges to detect material draw-in. Make corrective adjustments one parameter at a time to achieve repeatable results.
