
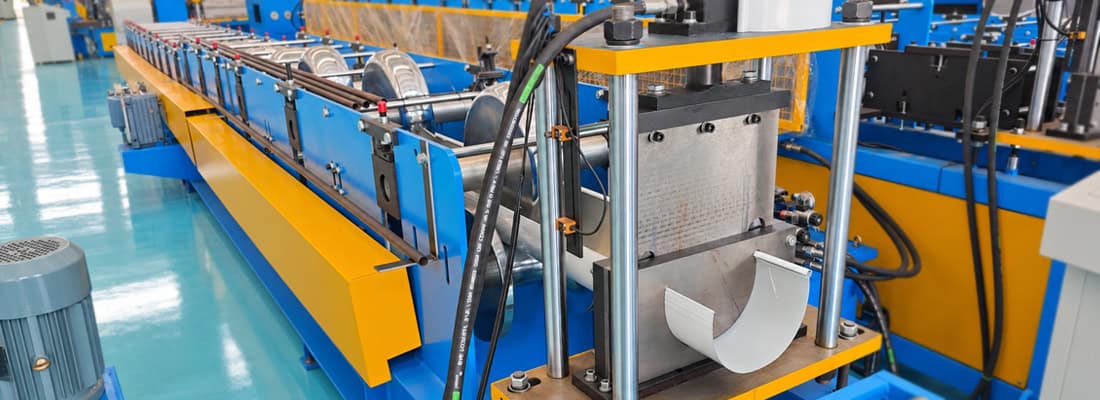
Why Half-Round Gutter Profiles Wrinkle?
Why Half-Round Gutter Profiles Wrinkle: Diagnosing Entry Guide Alignment and Roll Gap Imbalance
When a half-round rainwater gutter roll forming machine line starts producing wrinkled, wavy free edges, production engineers must separate cause from symptom quickly. The visible defect—compressive wrinkling along the unsupported strip edge—can originate from entry guide misalignment, roll gap imbalance, strip width variation, or insufficient leveling. Understanding how each of these factors interacts with the forming sequence is the first step toward correcting half round gutter roll forming wrinkling without wasting material on trial-and-error adjustments.
Table of Contents
Where Edge Wrinkles Occur in Half-Round Gutter Profiles
In half-round gutter roll forming, the profile develops its characteristic open semicircular shape progressively through a series of curved passes. The strip edges remain free and unsupported throughout most of the forming sequence—they only become part of the final hem or flange near the last stations. Edge wrinkles typically appear along these free edges, often between the third and seventh forming passes, as the radius tightens and the strip begins to work-harden.
Operators usually detect the defect as half round gutter edge waviness that runs parallel to the strip length. The wrinkles may be barely visible at the entry end, then become progressively more pronounced as the profile moves downstream. In severe cases, the edge develops a permanent distortion that remains visible in the finished gutter and can be felt by hand as a rippled surface.
Why Curved Gutter Passes Put the Strip Edge in Compression
The mechanics of roll forming a curved open profile place the strip edges in a fundamentally different stress state than flat or lightly profiled sections. As the center of the strip is forced downward into the roll cavity, the material along the outer edge must travel a different path length than the material at the centerline. The natural response of the strip is to resist this differential elongation.
When the roll gap at the edge is tighter than at the center, the edge material is driven outward and then compressed back as the strip attempts to equalize its length. This compressive stress, combined with the thin gauge typical of gutter stock, creates the conditions for buckling. The edge essentially has nowhere to release the excess material except by waving. This behavior explains why the problem is more common on deeper profiles and thinner materials, where the stiffness of the edge is insufficient to resist buckling.
How Entry Guide Misalignment Feeds Uneven Strip Tracking
Gutter roll forming guide alignment plays a decisive role in controlling where the strip enters the first pass. If the entry guides are set too tight on one side, or if the guide centerline does not match the pass centerline, the strip will track asymmetrically into the rolls. One edge will therefore receive more forming work than the other.
This asymmetry creates uneven elongation between the two free edges. The edge that travels through the tighter side of the forming zone is stretched more severely, then wrinkles as it relaxes downstream. Operators often mistake the resulting defect for a roll gap problem because the wrinkles appear on both edges, even though the root cause is simply a strip that is not entering the line straight.
A useful diagnostic clue is to compare the wrinkle pattern on both edges. If one edge is consistently worse, guide misalignment is likely. If both edges wrinkle equally and simultaneously, the cause is more probably distributed across the pass geometry. Checking the strip against the entry side guides with a feeler gauge, while the line is stopped, quickly reveals whether the guides are pinching one side or allowing lateral drift.
Roll Gap Imbalance vs Guide Misalignment: Diagnostic Checks
To avoid guesswork, perform the following checks in sequence when half round gutter roll forming wrinkling appears:
- Measure strip width at three points along 1 meter of coil and compare against the pass design allowance. Narrow or varying strip width will starve the edge support.
- Verify that the strip enters the first and second passes perfectly on the pass centerline. Use a straightedge and mark the strip edge at two stations to confirm tracking.
- Check the roll gap across each pass with a feeler gauge while the rolls are closed but not under load. The gap should be even left-to-right and match the design gap for the material thickness.
- Inspect the roll surfaces for localized wear or buildup at the edge region, which can simulate an imbalance even when the setup is correct.
- Run a single test strip at reduced speed and observe both edges at the exit of each pass to locate the exact station where waviness initiates.
The following table summarizes how to separate the likely causes based on observable strip behavior:
| Observed Condition | Likely Cause | Primary Check |
|---|---|---|
| Wrinkles appear on one edge only | Entry guide misalignment causing asymmetric tracking | Verify strip enters first pass on centerline; check guide contact on both sides |
| Wrinkles appear equally on both edges while strip tracks straight | Roll gap imbalance or pass geometry issue | Measure roll gap left-to-right with feeler gauge against design clearance |
| Strip drifts laterally during forming | Entry guide misalignment or excessive guide clearance | Confirm guide centerline matches pass centerline; check for side play |
| Edge support starved despite correct tracking | Strip width variation from coil | Measure strip width at multiple points along coil length |
| Waviness magnified through curved passes | Residual edge waves from slitter or coil set | Inspect incoming strip condition; verify leveling removes edge waves |
This sequence separates the dominant cause without guesswork. If the strip is tracking straight but wrinkles appear simultaneously on both edges, roll gap imbalance or pass geometry is the responsible variable. If the strip drifts laterally, guide alignment is the primary suspect.
Corrective Adjustment of Entry Guides and Roll Gaps
Correcting guide misalignment begins with loosening the entry guide mounting and establishing the true pass centerline using the bottom roll of the first station as reference. Set the guides so they contact the strip edge lightly on both sides with zero side play, then lock them down. Verify the setting by feeding a short strip through at crawl speed and checking for lateral movement at the exit of the first pass.
For roll gap adjustment, loosen the eccentric adjustment screws on the driven side and the operator side equally. Bring the gaps down progressively, measuring after each small adjustment, until the gap matches the designed clearance. Downspout roll forming adjustment follows a similar principle: reset the gap to the specified tolerance, then make small incremental changes rather than large swings. Avoid the temptation to tighten one side to correct a wrinkle on the opposite edge—this usually shifts the problem rather than solving it.
After making adjustments, run 2–3 meters of test strip at normal line speed and inspect both free edges for waviness. Compare the result with the previous test strip before making another small adjustment.
When Strip Width and Leveling Must Be Checked
Entry guides and roll gaps are not the only contributors to gutter roll forming defects. If the incoming coil has excessive width variation, the strip may lose proper edge contact with the guide rollers in the first pass, allowing the forming loads to push the strip sideways. Narrow strip sections reduce the material available to form the edge hem, which lowers the local stiffness and promotes buckling under compression.
Insufficient leveling is another common contributor. Coil set or edge waves from the slitter are not always removed before forming. When a strip with residual edge waves enters a curved forming sequence, the existing waviness becomes magnified as the profile radius tightens. Passing the strip through a precision leveler to reduce edge wave amplitude before it reaches the entry guides can eliminate the defect source even when guide alignment and roll gaps are correct.
A reliable half round gutter machine troubleshooting combines consistent strip width control with routine leveling, keeping the material condition predictable so the forming line variables remain isolated for diagnosis. The roll forming process is generally well understood, and recognized engineering references describe similar edge stability concerns in other open profiles, reinforcing that these checks apply broadly across roll forming practice.
Resolving half round gutter roll forming wrinkling depends on disciplined diagnosis. When the strip tracks straight and the material is clean and level, guide misalignment and roll gap imbalance can be isolated and corrected precisely. Once those variables are in control, the free edge of every gutter profile should follow the roll contour without compressive buckling, producing consistent, saleable sections pass after pass.
Frequently Asked Questions
How do I identify if guide misalignment causes wrinkling? ›
Check if the wrinkles appear predominantly on only one edge of the half-round gutter profile. If they do, the strip is likely tracking asymmetrically into the first forming pass, which is the pre-dominant symptom of entry guide misalignment. Verify the guide centerline matches the pass centerline and that both sides contact the strip lightly with zero side play.
How do I check roll gap balance across a pass? ›
To check for roll gap imbalance, stop the line and close the rolls without material. Use a feeler gauge to measure the gap on the left and right sides of each pass. The gap should be even across the full profile width and match the designed clearance for the material thickness you are running. Uneven gaps force one edge to do more work, causing compressive wrinkling.
Can incoming strip width variation cause edge wrinkles? ›
Yes. If the coil width varies beyond the pass design allowance, the strip loses consistent contact with the entry side guides. This starves the edge of proper support and lowers its local stiffness, making it far more susceptible to buckling and wavy free edges during the curved forming process. Measure strip width at multiple points along a meter of coil to verify consistency.
What is the difference between an edge wave and a wrinkle? ›
An edge wave is typically a pre-existing condition in the incoming strip, often left by a slitter or coil set, while a wrinkle is a new defect created during forming due to compressive forces. If your entry guides and roll gaps are correct but waviness still appears, inspect the incoming material. The existing edge wave is likely being magnified as the profile radius tightens.
Why do wrinkles appear only after several forming passes? ›
In half-round gutter roll forming, the strip edges remain free and unsupported during the early stations. Between the third and seventh passes, the radius tightens and the material begins to work-harden significantly. This is when the differential path lengths between the center and the edges create enough compressive stress to cause visible buckling along the unsupported edge.
How do I know if a wrinkle is from tooling or material? ›
A systematic check helps isolate the cause. First, confirm the strip is entering straight and the roll gaps are balanced. If the strip tracks straight and wrinkles appear equally on both edges, the cause is likely tooling, specifically pass geometry. If those factors check out, the problem likely lies in material condition, such as residual edge waves that require leveling.
Should I adjust only the tight side to fix a one-side wrinkle? ›
No. Tightening or loosening an adjustment on a single side usually shifts the problem rather than solving it, and can introduce asymmetric stresses that cause the strip to curve or bow. Correctly diagnosing gutter roll forming guide alignment and roll gap imbalance is essential. Make small, incremental adjustments to the eccentric screws on both the driven and operator sides of the line.
