
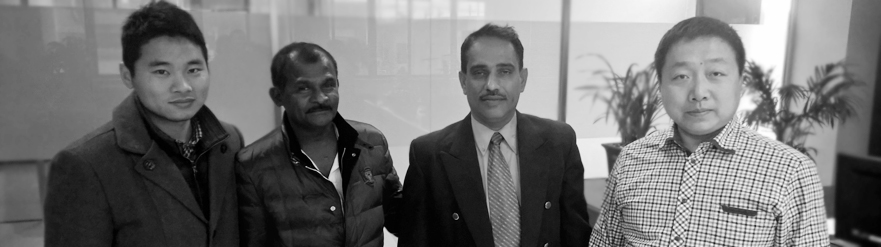
Client From Sri Lanka Visited MAXON for the Order of Roll Formers
Mr. Senarath Bandara and Mr. Ajith Wickramarachchi visited MAXON yesterday morning to discuss face to face about the order of roll formers and some auxiliary equipments, like slitting machine and curving machin etc.
This client is looking for high quality equipments and there are four roll forming machines required, i.e. quick change c/z purlin roll forming machine, metal roof tile roll forming machine, roof panel roll forming machine and wall cladding roll forming machine, and also a mini slitting machine and hydraulic crimping curved machine are also required.

The raw material the client is going to use is G550 colour steel for the propduction of roof panel and wall cladding, and the material width is 940mm and thickness is 0.3-0.5mm; for metal roof tiles, the material will be G350 colour steel with 1220mm width and 0.45mm thickness, and for c & z steel purlins, the material is Cold rolled steel and galvanized steel with 1.6-3mm thickness.
The interchangeable c and z steel purlin roll forming machine consists of a manual decoiler, leveler, transmission system (hydraulic transmission), roll forming system, quick-change system, punching and cutting system and control system; this machine produces different c and z steel purlins without changing anything. All the operation or action could be done through the PLC computer control system, except only for the quick change from C to Z (only around 10 minutes).
The roof panel roll forming machine and wall cladding roll forming machine are the simplest machines with components manual decoiler, roll foring part, transmission part, hydraulic system, cutting system and control system, and the metal roof tile roll forming machine has an extra punching system.
Frequently Asked Questions
What roll forming machines and auxiliary equipment were ordered by the Sri Lankan client? ›
The client ordered four roll forming machines: a quick change C/Z purlin machine, a metal roof tile machine, a roof panel machine, and a wall cladding machine. They also required a mini slitting machine and a hydraulic crimping curved machine to support their production line. These machines are intended to produce various building components from color-coated steel coils.
What raw materials and specifications are suitable for the roof panel and wall cladding machines mentioned on this page? ›
For roof panel and wall cladding production, the client plans to use G550 color steel. The material width is 940 mm, and the thickness ranges from 0.3 to 0.5 mm. To get a precise quote or configuration, you should confirm your specific material grade, yield strength, coating type, and coil inner diameter, as these factors affect roller design and machine setup.
What material specifications apply to the metal roof tile roll forming machine for this project? ›
The metal roof tile machine in this order will process G350 color steel with a strip width of 1220 mm and a thickness of 0.45 mm. However, your own requirements may vary. The machine’s forming rollers and punching stations need to be matched to your exact tile profile and material properties. We recommend submitting your material samples or detailed specifications for a machine compatibility check.
Which materials are compatible with the quick change C/Z purlin roll forming machine? ›
For purlin production, this machine is set up to run cold-rolled steel and galvanized steel with thicknesses from 1.6 mm up to 3 mm. The quick-change system allows the same machine to switch from C purlins to Z purlins without changing rollers. Your coil width and yield strength must be within the machine’s design range. Contact us with your specific profile dimensions to confirm suitability.
How does the quick-change system work on the C/Z purlin machine, and what is involved in switching profiles? ›
This C/Z purlin machine is designed to produce both C and Z purlins without physical roller changes. The profile changeover is controlled through the PLC system, and the only manual step is the quick-change mechanism, which can be completed in about 10 minutes. All punching, cutting, and forming actions are automated. This design minimizes downtime and increases production flexibility.
What are the typical components and control systems included in these roll forming machine configurations? ›
Based on the described order, each machine includes a manual decoiler, a leveling unit (where applicable), a roll forming section, and a hydraulic cutting system. The roof panel and wall cladding machines have simple PLC controls. The purlin machine features hydraulic transmission and a full PLC system for all functions except the quick-change operation. The metal roof tile machine also includes an additional punching system. The exact configuration depends on your production needs.
What factors should I consider when planning production speed and output for a line like the one ordered by the Sri Lankan client? ›
Production speed depends on material thickness and grade, profile complexity, the number of punching operations per part, and cut length accuracy. For example, thinner gauge steel (0.3 to 0.5 mm) can be formed faster than heavier gauge material (1.6 to 3 mm). Your required output volume and available operator skill levels should be discussed with our engineers to set realistic line speed and automation levels during the Quotation stage.
